
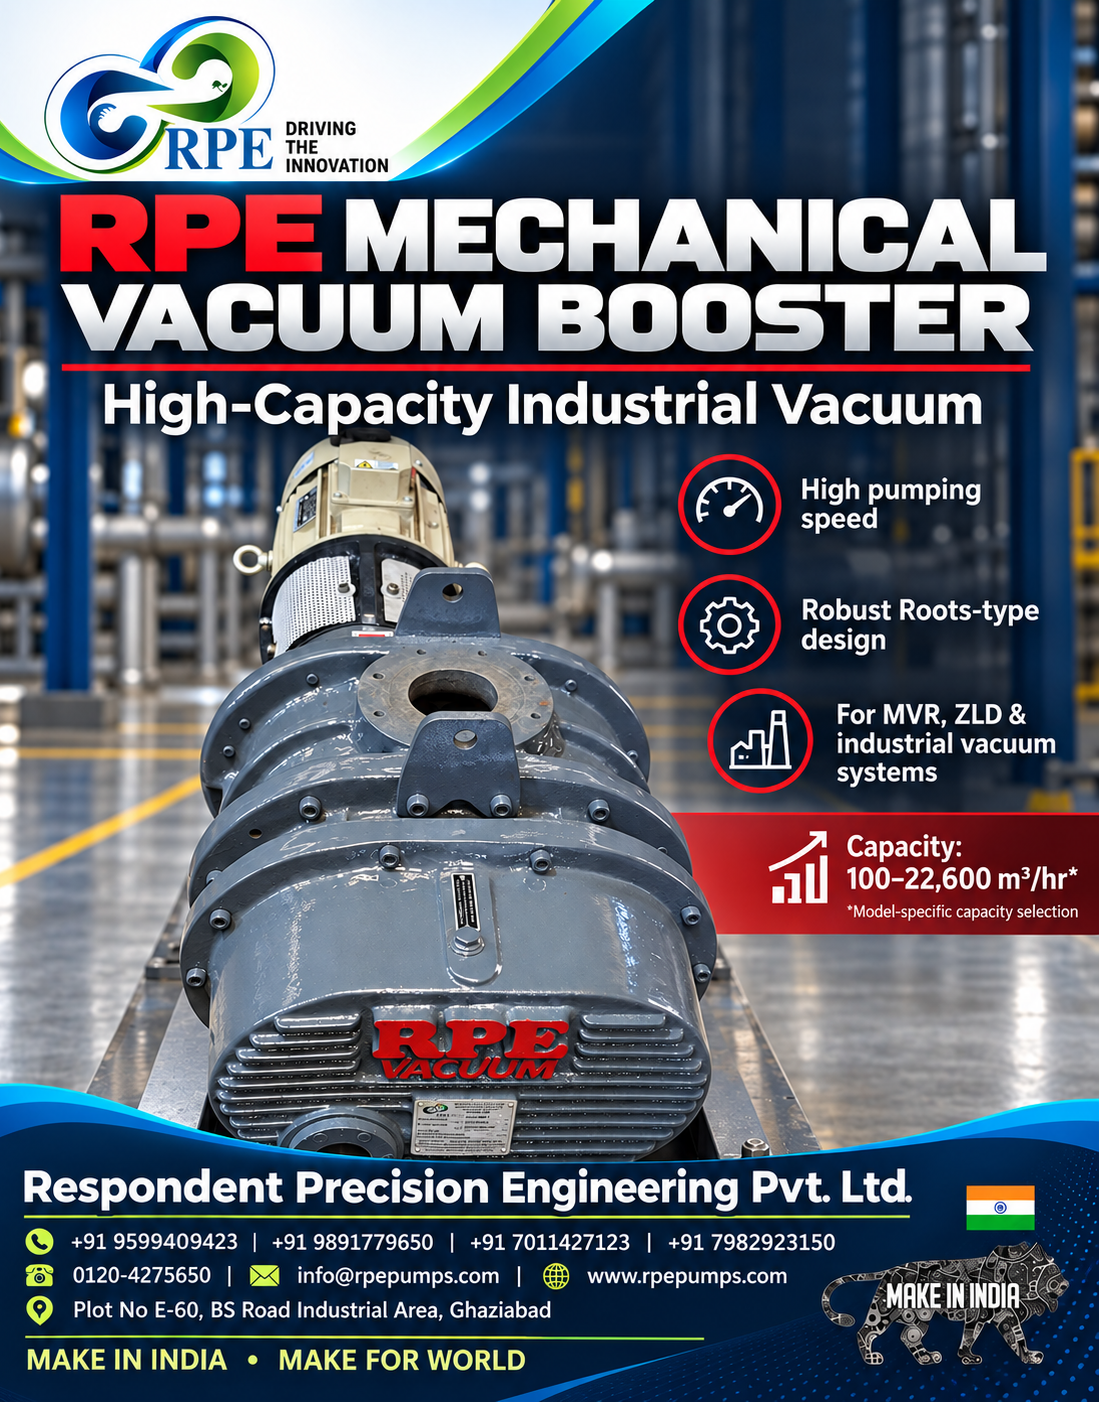
RPE mechanical vacuum boosters for vacuum distillation, solvent recovery, filtration and drying. Share your process conditions for model selection. Mechanical Vacuum Boosters for Industrial Vacuum Applications Industrial processes such as vacuum distillation, solvent recovery, filtration and drying need a vacuum system suited to their operating conditions. A mechanical vacuum booster can help increase the pumping speed of a vacuum system when selected and operated with a suitable backing pump. Respondent Precision Engineering Private Limited, or RPE, manufactures mechanical vacuum boosters for a range of industrial vacuum applications. What does a mechanical vacuum booster do? A mechanical vacuum booster is a positive displacement machine. It uses two counter rotating lobed rotors to move gas from the suction side toward the discharge side. Timing gears keep the rotors in position, while small operating clearances support the pumping action. The gas path does not require internal rotor lubrication. A booster is generally used as part of a vacuum system with a backing pump. The correct combination depends on the required pumping speed, suction pressure, discharge pressure, gas composition, temperature and process duty. Sharing these details helps the engineering team assess a suitable configuration for the application. Applications of RPE mechanical vacuum boosters RPE mechanical vacuum boosters are used in vacuum systems for applications including: • Solvent recovery • Vacuum distillation • Vacuum filtration • Degassing of molten polymers • Drying of heat sensitive powders, active pharmaceutical ingredients and intermediates • Transformer oil dehydration • Surface coating processes, including titanium nitride, chrome and diamond like coatings • Zero Liquid Discharge systems, in combination with a suitable water ring or dry screw backing pump Each process has different gas loads and operating requirements. Selecting a booster by capacity alone may not be sufficient. A review of the operating conditions helps identify a suitable booster and backing pump arrangement. Model wise capacity and system selection RPE’s August 2025 product catalogue lists mechanical vacuum booster displacements from 260 to 15, 100 cubic metres per hour at 1500 rpm and 50 Hz. The catalogue also lists 60 Hz values for the two largest models. Actual selection is model specific and depends on the required vacuum level, system pressure, backing pump capacity and process conditions. Before requesting a recommendation, prepare the following details: • Required pumping speed or process load • Suction pressure or target vacuum • Discharge pressure • Gas or vapour composition and temperature • Whether the duty is continuous or intermittent • Existing or proposed backing pump details • Power supply and any hazardous area requirement These inputs help evaluate the booster within the complete vacuum system. RPE engineering and support RPE is an engineering and manufacturing company based in Ghaziabad, India. Its portfolio includes mechanical vacuum boosters, roots blowers, vacuum systems, water ring vacuum pumps, acoustic enclosures and related spare parts. RPE also provides service support for vacuum boosters and other equipment in its portfolio. If you are planning a new installation, improving an existing vacuum system or replacing a booster, share your process data with RPE. The team can review the application and help identify a suitable model and system arrangement. Discuss your application with RPE: Respondent Precision Engineering Pvt. Ltd. +91 9599409423 | +91 9891779650 | +91 7011427123 | +91 7982923150 0120-4275650 | info@rpepumps.com | www.rpepumps.com Plot No E-60, BS Road Industrial Area, Ghaziabad Make in India • Make for World #MechanicalVacuumBooster #VacuumBooster #VacuumTechnology #VacuumDistillation #SolventRecovery #IndustrialVacuum #MVR #ZLD #IndustrialEngineering


This is your website preview.
Currently it only shows your basic business info. Start adding relevant business details such as description, images and products or services to gain your customers attention by using Boost 360 android app / iOS App / web portal.
Vacuum Booster Manufacturer
2026-10-07T05:55:15
RPE mechanical vacuum boosters for vacuum distillation, solvent recovery, filtration and drying. Share your process conditions for model selection. Mechanical Vacuum Boosters for Industrial Vacuum Applications Industrial processes such as vacuum distillation, solvent recovery, filtration and drying need a vacuum system suited to their operating conditions. A mechanical vacuum booster can help increase the pumping speed of a vacuum system when selected and operated with a suitable backing pump. Respondent Precision Engineering Private Limited, or RPE, manufactures mechanical vacuum boosters for a range of industrial vacuum applications. What does a mechanical vacuum booster do? A mechanical vacuum booster is a positive displacement machine. It uses two counter rotating lobed rotors to move gas from the suction side toward the discharge side. Timing gears keep the rotors in position, while small operating clearances support the pumping action. The gas path does not require internal rotor lubrication. A booster is generally used as part of a vacuum system with a backing pump. The correct combination depends on the required pumping speed, suction pressure, discharge pressure, gas composition, temperature and process duty. Sharing these details helps the engineering team assess a suitable configuration for the application. Applications of RPE mechanical vacuum boosters RPE mechanical vacuum boosters are used in vacuum systems for applications including: • Solvent recovery • Vacuum distillation • Vacuum filtration • Degassing of molten polymers • Drying of heat sensitive powders, active pharmaceutical ingredients and intermediates • Transformer oil dehydration • Surface coating processes, including titanium nitride, chrome and diamond like coatings • Zero Liquid Discharge systems, in combination with a suitable water ring or dry screw backing pump Each process has different gas loads and operating requirements. Selecting a booster by capacity alone may not be sufficient. A review of the operating conditions helps identify a suitable booster and backing pump arrangement. Model wise capacity and system selection RPE’s August 2025 product catalogue lists mechanical vacuum booster displacements from 260 to 15, 100 cubic metres per hour at 1500 rpm and 50 Hz. The catalogue also lists 60 Hz values for the two largest models. Actual selection is model specific and depends on the required vacuum level, system pressure, backing pump capacity and process conditions. Before requesting a recommendation, prepare the following details: • Required pumping speed or process load • Suction pressure or target vacuum • Discharge pressure • Gas or vapour composition and temperature • Whether the duty is continuous or intermittent • Existing or proposed backing pump details • Power supply and any hazardous area requirement These inputs help evaluate the booster within the complete vacuum system. RPE engineering and support RPE is an engineering and manufacturing company based in Ghaziabad, India. Its portfolio includes mechanical vacuum boosters, roots blowers, vacuum systems, water ring vacuum pumps, acoustic enclosures and related spare parts. RPE also provides service support for vacuum boosters and other equipment in its portfolio. If you are planning a new installation, improving an existing vacuum system or replacing a booster, share your process data with RPE. The team can review the application and help identify a suitable model and system arrangement. Discuss your application with RPE: Respondent Precision Engineering Pvt. Ltd. +91 9599409423 | +91 9891779650 | +91 7011427123 | +91 7982923150 0120-4275650 | info@rpepumps.com | www.rpepumps.com Plot No E-60, BS Road Industrial Area, Ghaziabad Make in India • Make for World #MechanicalVacuumBooster #VacuumBooster #VacuumTechnology #VacuumDistillation #SolventRecovery #IndustrialVacuum #MVR #ZLD #IndustrialEngineering
2026-10-07T05:55:15


Submit Your Enquiry